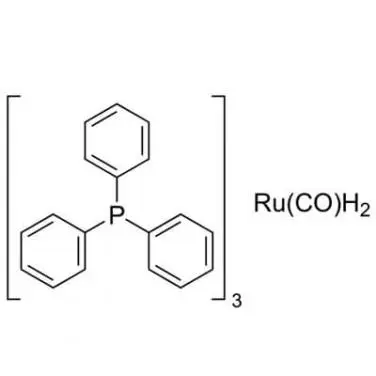
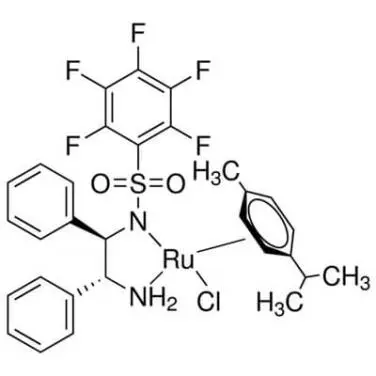
We specialize in precious metal catalysts, integrating R&D, large-scale production and strict QC to provide stable customized products and efficient global delivery for global industrial customers.
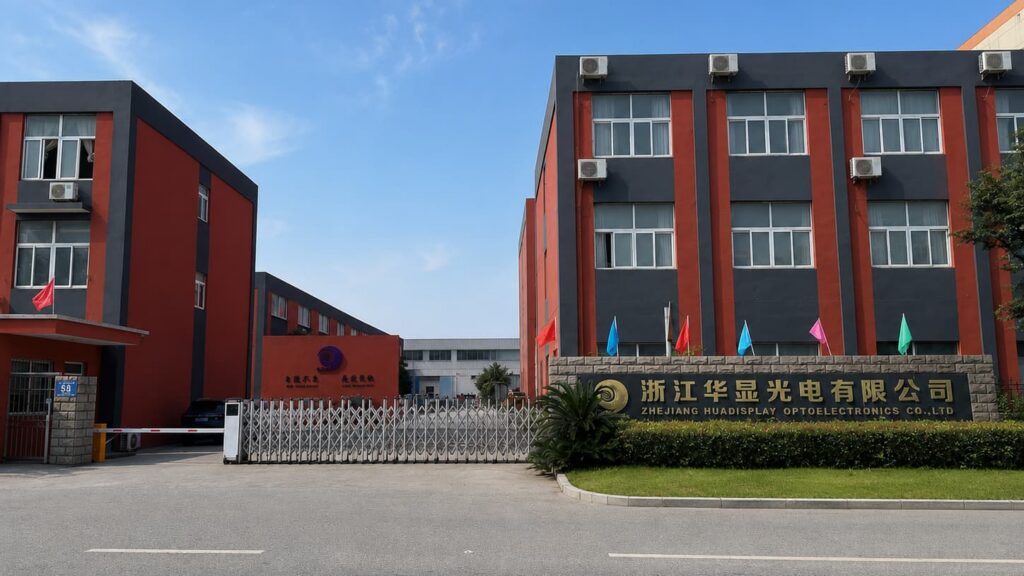
Founded in 2009, UIV CHEM has grown steadily. We set up Zhejiang Huaxian Optoelectronics in 2016 with investment from top institutions. Our seasoned team with 15+ years’ Precious Metal Catalyst experience masters mass production and patent development. We own over 140 patents and hold many prestigious honors including National Little Giant Enterprise, with academician and postdoctoral workstations. Our proprietary materials supply major domestic panel firms, ranking us a leading Precious Metal Catalyst supplier.
yurui(Shanghai) is the group’s global sales and marketing center, specializing in precious metal catalysts, pharmaceutical intermediates, ligands, and specialty chemicals. With products exported to more than 100 countries and regions, we provide efficient supply chain management, responsive technical support, and customized solutions for customers worldwide.
Zhejiang Huaxian
R&D Center
Zhejiang Huaxian is the group’s research and development center and a National High-Tech Enterprise. The company has established a Provincial Enterprise Research Institute, Postdoctoral Workstation, and Academician Workstation. Backed by an experienced R&D team, it has developed synthesis processes for 2,000+ products and provides customized development and process optimization services.
Anhui Huaxian
Manufacturing Base
Anhui Huaxian is the group’s manufacturing base, covering 66,667 m² with 200+ reactors (500–10,000 L). Operating under certified quality management systems, the facility delivers reliable scale-up and commercial production with stable quality, flexible manufacturing, and dependable global supply.
Why Choose UIV
At UIV CHEM, you’re not just choosing a material supplier—you’re choosing a long-term partner in innovation and precision. With a vertically integrated supply chain and strong R&D capabilities, we deliver cutting-edge chemical solutions from lab to large-scale production.
Veteran Expert R&D Team
Core team with 15+ years of experience, backed by postdoctoral and academician-level expertise.
Full Chain for Five Core Products
Full Industry Chain Coverage: From raw materials to end products across photoresists, silicone, resins, polyimide, and cleaning solutions.
Lab to ton production, fully customized
Lab-scale samples to ton-level production—tailored to your process needs.